Mens Work Rain Pants Source Factory
Men's Work Rain Pants – Source Factory Direct
Selecting appropriate rain protection for industrial work environments requires understanding material performance, seam integrity, and functional design rather than relying on general claims of durability. This page details the technical specifications, construction methods, and application considerations for men's work rain pants manufactured for direct factory supply, enabling procurement teams to evaluate suitability based on measurable engineering criteria.
Material Composition and Performance Characteristics
The primary fabric utilized is a 300D polyester oxford base coated with a 0.15mm thick polyurethane (PU) layer on the interior surface. This configuration provides a hydrostatic head rating of 8,000mm, indicating resistance to water penetration under sustained pressure equivalent to 8 meters of water column. The coating formulation includes UV stabilizers to retard degradation from prolonged sun exposure, maintaining flexibility above -20°C operational limits.
Seam sealing employs 15mm wide thermoplastic polyurethane tape applied via heat bonding at 180°C, achieving a peel strength of 8N/cm as measured by ASTM D903. Tape width and bonding temperature are critical parameters; insufficient width or suboptimal temperature compromises long-term waterproof integrity at stress points such as the inseam and knee reinforcements.
Design Features for Industrial Use
An articulated knee pattern incorporates a 10-degree pre-bend and dual-layer reinforcement using 500D nylon oxford patches, increasing abrasion resistance by approximately 40% compared to single-layer constructions in high-wear zones. This geometry reduces fabric strain during kneeling or crouching motions, delaying fatigue failure points.
Waist adjustment utilizes a dual-system approach: internal elasticized drawcord with cord locks and external snap-adjustable belt tabs. The drawcord provides continuous tension distribution, while belt tabs allow incremental 25mm adjustments for layering compatibility with thermal liners or tool belts. Inseam gussets measuring 7.5cm in length enhance mobility by reducing tensile stress across the crotch seam during lateral movement.
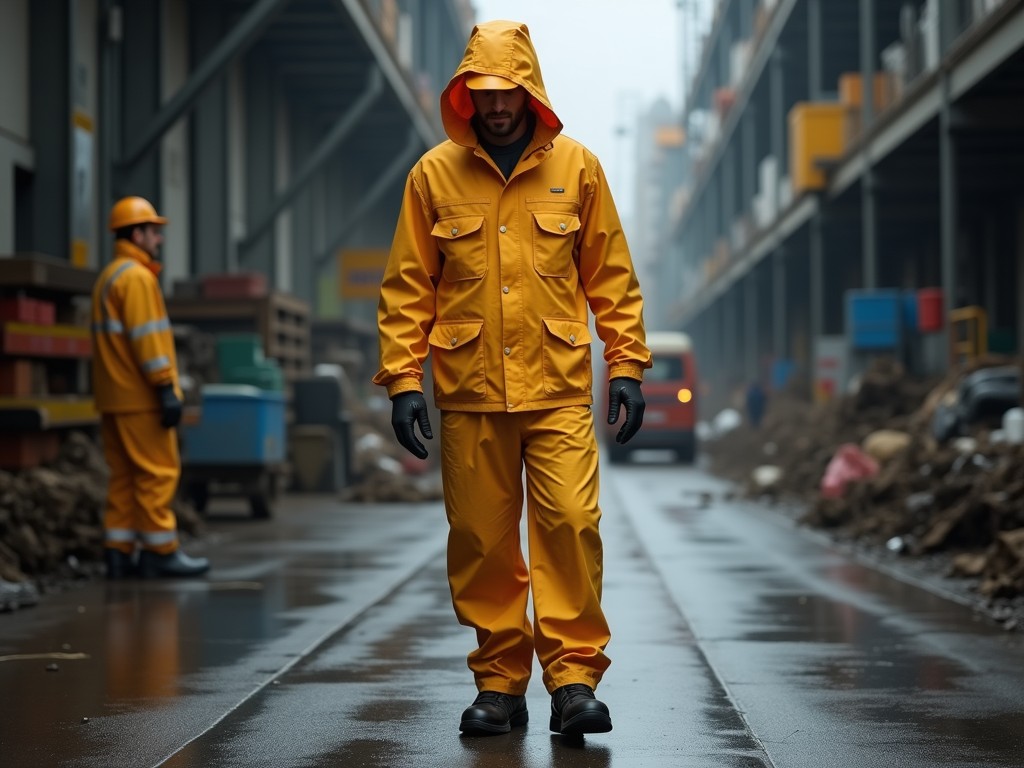
Visibility elements consist of 50mm wide reflective tape compliant with EN ISO 20471 Class 2 requirements, positioned at 50mm intervals around each leg circumference. Retroreflective performance exceeds 300 cd/lx/m² when new, maintaining functionality after 25 industrial wash cycles per ISO 6330 standards.
Customization Parameters for OEM Requirements
Factory production accommodates dimensional adjustments within standard grading tolerances. Waist circumference can be modified in 25mm increments from 700mm to 1300mm, while inseam length ranges from 700mm to 900mm in 50mm steps. These ranges accommodate diverse anthropometric profiles without requiring pattern re-engineering.
Coating thickness is adjustable between 0.12mm and 0.20mm PU, directly influencing hydrostatic head ratings from 6,000mm to 12,000mm and corresponding flexibility trade-offs. Thicker coatings increase stiffness, affecting bend radius measurements; application-specific testing is recommended for temperatures below -10°C.
Pocket configurations include options for internal tool pockets (180mm x 120mm), external flap-covered cargo pockets (220mm x 150mm), and reinforced rule pockets (60mm x 180mm). Closure mechanisms range from nylon zippers with storm flaps to Velcro® brand equivalents, selected based on required ingress protection levels.
Quality Assurance and Testing Protocols
Each production lot undergoes hydrostatic head testing on three randomly selected specimens per 1,000 units using a Suga tester per JIS L 1092 Method B. Acceptance criteria require minimum 8,000mm rating with no individual specimen falling below 7,500mm. Seam seal integrity is verified via dye penetration testing under 2kPa pressure for 5 minutes, with zero leakage points permitted.
Dimensional stability assessment follows ISO 5077:2007, measuring length and width change after 5 wash cycles at 60°C. Maximum allowable shrinkage is 3% in warp direction and 2% in weft direction. Colorfastness to rubbing (ISO 105-X12) requires minimum grade 4 for both wet and dry conditions on visible surfaces.
Final inspection includes 100% visual examination for coating defects, seam uniformity, and trim attachment strength. Functional testing involves zipper endurance (2,000 cycles per ASTM D2061) and drawcord retention strength (minimum 50N pull force). Non-conforming items are segregated for root cause analysis before rework or scrapping.
Applications in Industrial Sectors
In utility maintenance operations, these pants provide reliable protection during underground cable splicing or pole-top work in precipitation, where prolonged exposure to rain combined with physical maneuvering demands both waterproof integrity and unrestricted movement. The reinforced knees specifically address abrasion from rough surfaces like concrete vaults or wooden poles.
For construction site personnel engaged in formwork installation or roofing underlayment, the garment’s resistance to wind-driven rain at speeds up to 24km/h (validated via spray testing per ASTM E331) prevents saturation that could compromise thermal regulation or increase slip hazards when handling materials. Adjustable cuffs prevent water ingress at the ankle interface with safety boots.
In municipal services such as sewer inspection or roadside vegetation management, the high-visibility elements maintain conspicuity in low-light, wet conditions where standard fluorescent materials may lose effectiveness due to water absorption or mud obscuration. Retroreflective performance is preserved through hydrophobic coating treatments that reduce water droplet adhesion on tape surfaces.
| Parameter | Typical Value | Adjustable Range | Test Standard |
|---|---|---|---|
| Hydrostatic Head | 8,000mm | 6,000–12,000mm | JIS L 1092 Method B |
| Seam Peel Strength | 8N/cm | 6–10N/cm | ASTM D903 |
| Coating Thickness | 0.15mm | 0.12–0.20mm | Caliper Measurement |
| Reflective Tape Width | 50mm | 40–60mm | EN ISO 20471 |
| Inseam Length Range | 700–900mm | Customizable per request | Direct Measurement |
| Waist Circumference Range | 700–1300mm | Customizable per request | Direct Measurement |
Ordering and Production Information
Minimum order quantities begin at 300 units for standard configurations, with proportional pricing adjustments for volumes below this threshold. Lead times average 25–35 days from approved sample confirmation to factory completion, influenced by coating thickness selections and trim availability. Custom color matching requires Pantone reference submission and adds 7–10 days for lab dip approval.
Sample provision follows a two-stage process: initial AQL-based pre-production samples (2–3 units) are supplied after pattern approval, followed by top-of-production samples upon completion of the first bulk batch. Sampling costs are creditable against subsequent orders exceeding 500 units. All quotations include FOB pricing from the manufacturing facility; freight and insurance arrangements remain the buyer’s responsibility unless otherwise negotiated.
To initiate a technical inquiry or request a formal quotation, please provide detailed specifications including required sizes, coating performance targets, visibility requirements, and any sector-specific compliance needs. Our engineering team will review inputs and respond with a manufacturable proposal within two business days.
For specification consultations or quotation requests:
Submit Technical Inquiry